Every machine shop has that one magical moment when a problem stops looking expensive and starts looking solvable. You stare at the part, glance at the tool rack, ignore the voice whispering “buy more accessories,” and realize the answer has been sitting on the bench the whole time. That is the spirit behind “Indexing Chuck Not Required.” It is not anti-tool, anti-precision, or anti-common sense. It is the wonderfully stubborn idea that you do not always need a dedicated indexing chuck or full dividing setup to make clean, repeatable indexed features.
In practical terms, indexing means rotating a workpiece by a specific amount between cuts so features land in evenly spaced positions. That sounds fancy, but the basic examples are everywhere: flats on a bolt head, finger notches on a knob, flutes on a column, equally spaced holes around a round part, and simple gear-like layouts. In many shops, the default solution is a dedicated indexing attachment, rotary table, dividing head, or spin jig. Those are great tools. They exist for a reason. But they are not always the first answer, the cheapest answer, or even the smartest answer for a one-off piece.
The better question is this: How accurate does the job need to be, and what geometry do you already have? That question turns a routine machining task into a creative one. And sometimes, that creativity beats complexity with one hand tied behind its back.
What “Indexing Chuck Not Required” Really Means
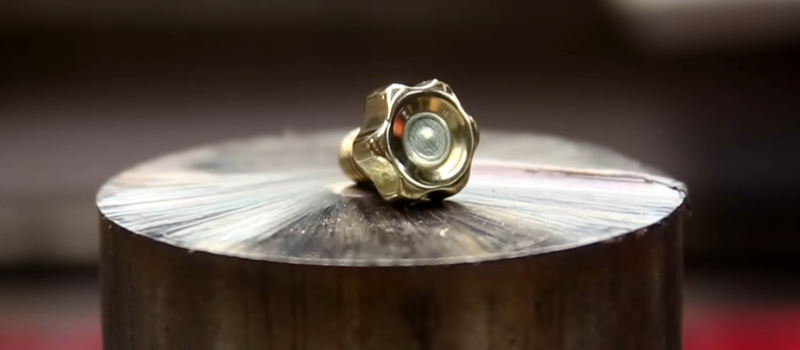
The phrase became memorable because it captures a very specific kind of workshop cleverness. Instead of using a purpose-built indexing chuck, you exploit the geometry of an ordinary material or setup to create repeatable positions. A classic example is using hex stock as an instant six-position index. Those six flats are not decoration. They are built-in reference surfaces. Rotate from flat to flat, lock the work, and you have six evenly spaced orientations without needing a dedicated indexing chuck.
That simple idea matters because machining is not only about horsepower and hardware. It is about constraint. When a part needs six knurled-like finger notches, six side cuts, or six evenly placed features, a machinist can often let the stock shape do part of the thinking. Hex brass, hex steel, or hex aluminum can become part material, part fixture, and part strategy. That is workshop thrift at its finest: fewer setups, fewer custom fixtures, and fewer reasons to spend half the day inventing a problem for your wallet.
There is also a mindset hidden inside the title. “Not required” does not mean “never useful.” It means the shop should not reach for maximum complication when modest precision will do the job beautifully. If the feature count matches the stock geometry, or if the part can be indexed off existing holes, grooves, flats, or stops, the expensive route may simply be overkill wearing a very serious face.
Why Indexing Matters in the First Place
Indexed machining shows up whenever symmetry matters. If one notch is deeper than the others, or one flute lands a few degrees off, the part stops looking intentional and starts looking homemade in the wrong way. There is “handcrafted,” and then there is “why is this knob lopsided?” The first sells. The second becomes a lesson.
That is why dedicated indexing tools are so popular. An indexing attachment can rotate a workpiece in controlled increments. A dividing head can handle precise spacing patterns for gears, circular hole patterns, and repeated radial features. A spin jig can provide direct indexing in fixed steps and fine angular adjustment. Rotary tables with dividing plates add another option for circular positioning. These tools are fantastic when you need repeatability, formal accuracy, or production-friendly workflow.
Still, not every task deserves the full ceremony. Milling flats on a custom bolt head is not the same as cutting precision gear teeth. Cutting six decorative grip notches on a thumb screw is not the same as machining aerospace parts that will later lecture you about tolerance stack-up. The job decides the method, not the other way around.
Smart Alternatives to a Dedicated Indexing Chuck
1. Use Stock Geometry as Your Index
This is the hero move. Hex stock gives you six positions. Square stock gives you four. Even parts that already have flats or reference faces can be repositioned consistently if the setup is thoughtful. For custom knobs, bolts, and thumb screws, this can be all you need. The material shape becomes a low-tech indexing system hiding in plain sight.
The beauty here is not just cost savings. It is also setup speed. A machinist working on a one-off part often loses more time building the perfect fixture than cutting the actual part. If the raw stock already offers evenly spaced flats, you can use those flats to lock orientation, make a cut, rotate, and repeat. No elaborate plate. No gear train. No dramatic sighing over accessory catalogs.
2. Index from Existing Holes, Grooves, or Chuck Features
Some lathes and turning setups can use indexing holes, grooves, or spindle features already present in the system. In woodturning, index wheels and simple pins are common for laying out flutes, reeds, and decorative patterns. In some cases, a chuck or faceplate already provides matching positions, which makes a separate wheel unnecessary. This is the shop equivalent of finding money in an old jacket, except the money is angular control.
3. Use a Simple Wraparound Layout
Not every indexing job starts with a machine accessory. For hand-guided or low-force decorative work, you can mark a circumference on paper, divide it into equal lengths, wrap it around the part, and transfer the spacing. This method is especially handy in woodturning and layout-heavy projects where the goal is clean visual spacing rather than industrial-grade rotational math. It is not glamorous, but neither is perfectionism that missed the deadline.
4. Use a Spin Jig, Rotary Table, or Dividing Head Only When the Work Demands It
There is a sweet spot between improvisation and overengineering. When the part calls for many divisions, fine angle control, gear teeth, splines, or exact repeating hole patterns, purpose-built tools earn their keep. Direct indexing plates, vernier adjustments, and rigid workholding reduce guesswork and improve repeatability. In other words, the dedicated tool becomes the adult in the room. The trick is knowing when to invite it.
Where the “No Indexing Chuck” Approach Works Best
This strategy shines in prototype work, repair work, hobby machining, small-batch custom parts, and decorative turning. It is excellent when the number of positions matches an obvious geometry: four flats, six notches, eight evenly spaced decorative cuts, and similar patterns. It also works well when the part is small, the material is cooperative, and the tool forces are modest.
One of the best examples is custom hardware. A thumb screw, ornamental bolt, control knob, or shop-made fastener can often be improved with indexed grip features. The part looks better, feels better in the hand, and suddenly seems like something from a catalog with a suspiciously confident price tag. That transformation is exactly why clever indexing work is so satisfying. You start with raw stock and end with hardware that looks intentional, premium, and just a little smug.
This method also makes sense in lean workshops. Not every garage shop, school lab, or maintenance room has a dividing head sitting around waiting for applause. But many do have hex bar, standard chucks, simple jigs, and enough patience to make smart use of both. When tools are limited, thinking becomes a consumable resource. Use it generously.
Where It Stops Being the Right Idea
Let us now defend reality. There are jobs where “indexing chuck not required” becomes “indexing chuck very much required, please stop being romantic.” Precision gears, splines, tight angular tolerances, repeated production runs, and high-value parts all push the shop toward formal indexing equipment. If a feature count does not match your stock geometry, if the rotational steps are odd, or if the tolerance is narrow enough to start arguments, a dedicated system is the safer play.
Another limit is rigidity. A clever setup that works for light cuts may become a terrible setup for aggressive cuts. That is especially true when interrupted cuts, side loads, or awkward workholding enter the picture. There is a fine line between “resourceful” and “the machine made a new sound and I do not care for it.”
Repeatability is the other dividing line. One successful part can be made with a clever improvised method. Ten identical parts often justify a more formal process. At some point, the money saved by improvising gets eaten by time, checking, rechecking, and quietly distrusting your own setup.
Safety Is Not Optional, Even When the Chuck Is
This topic has a fun, scrappy vibe, but safety is where the jokes stop clocking in. Any indexing strategy lives or dies by secure workholding. The workpiece must be clamped properly. The chuck key must come out immediately after tightening. The toolpath must be checked by hand before starting. Speeds should be conservative, especially for large or awkward parts. Guards matter. Clearance matters. So does resisting the ancient temptation to “just try one pass” before confirming the setup.
Improvised indexing should never mean improvised safety. If the work is oversized, marginally clamped, unsupported, or likely to shift under cutting load, slow down and rethink it. A clever fixture is still a fixture. It has to resist force, preserve alignment, and keep the operator out of the danger zone. Shop ingenuity is admirable. Shop heroics are mostly paperwork waiting to happen.
The Real Lesson: Use Geometry Before You Use Your Credit Card
The enduring appeal of “Indexing Chuck Not Required” is bigger than one trick with hex stock. It is a reminder that good machining is not just about buying the right accessory. It is about recognizing when the part, material, and setup already contain enough order to get the job done. Flat sides can become indexes. Holes can become stops. Existing features can become references. And a supposedly limited setup can produce beautiful results when the operator understands the geometry instead of fighting it.
That lesson scales beyond hobby work. In professional manufacturing, smart fixturing is often what separates elegant production from expensive chaos. The exact tools may differ, but the principle is the same: use the simplest reliable method that meets the requirement. When the requirement is modest, the simple method is often faster, cheaper, and surprisingly elegant.
So no, an indexing chuck is not always required. Sometimes the smartest setup is already sitting on the bench, looking ordinary and pretending not to be the answer. That is the charm of machining. Precision may be a science, but getting there often begins as a clever little crime against unnecessary complexity.
Common Shop Experiences Related to “Indexing Chuck Not Required”
One of the most relatable experiences around this topic is the moment a machinist realizes the accessory they thought they needed is not actually the bottleneck. The real bottleneck is usually confidence. Many people freeze at the phrase “indexed features” because it sounds like a job for specialized equipment, advanced calculations, and somebody named Dennis who has been machining since the moon landing. Then they look at the part, notice the stock is hex, and suddenly the whole operation becomes approachable. That shift, from intimidation to clarity, is one of the best feelings in the shop.
Another common experience is discovering that simple setups often teach more than fancy ones. When you index from a flat, a hole, a pin, or a paper layout, you become more aware of reference surfaces, workholding, and sequence. You start paying attention to how tiny errors sneak in. You learn why consistency matters. You feel the difference between a setup that merely holds and a setup that repeats. Those lessons stick, because they are earned the slightly annoying way: by doing the work twice when the first orientation was off by just enough to mock you.
There is also a familiar budget-shop experience behind this idea. Plenty of hobbyists, repair techs, and small-shop owners work in spaces where every tool purchase competes with material costs, measuring tools, and the general expense of being interested in metal. In those environments, the ability to improvise responsibly is not just charming; it is practical. Making a good part without buying a new indexing chuck feels like winning twice. You save money, and you gain skill. The machine does not care that the solution was humble. It only cares whether the setup was sound.
Then there is the cosmetic payoff. Many people try this kind of indexing method for functional reasons and end up hooked because the finished parts simply look better. A plain bolt becomes a thumb screw. A smooth cylinder becomes a fluted detail. A basic knob suddenly has grip, rhythm, and personality. The result looks designed instead of merely made. That visual transformation creates a lot of shop enthusiasm because it proves that small geometric choices can dramatically change how a part feels in the hand.
Of course, there is usually one humbling experience mixed in. Maybe the part slips. Maybe one notch ends up slightly wider. Maybe the operator forgets to deburr between steps and spends the rest of the afternoon pretending the scratch was “part of the process.” Those moments are normal. In fact, they are useful. They teach the boundary between clever and careless. And once that boundary becomes clear, the whole method gets better.
That is why this topic keeps resonating with makers and machinists. It is not just about skipping a specialized chuck. It is about developing the habit of seeing possibilities in ordinary geometry. After enough shop time, that habit becomes second nature. You stop asking, “What tool should I buy?” and start asking, “What reference do I already have?” That question is often where the best parts begin.